Cigarettes, pre-rolls, and loose leaf should not share one package size simply because the outside shape looks suitable. A tobacco tin for straight sticks follows length, row count, and layer depth, while tapered pre-rolls add insert geometry and removal space. Loose fill creates a different problem because settled volume and headspace matter more than a fixed product outline. Reliable sizing starts with the packed contents and works outward.
The Practical Answer
Size the usable internal cavity around the maximum packed product. Then account for inserts, loading clearance, removal access, headspace, closure movement, and the required outside carry profile.
Start With the Packed Envelope
Inputs That Determine Tobacco Tin Size
Outside length and width are often the easiest dimensions to discuss at the beginning of a packaging project. However, those numbers do not describe how the contents actually sit inside the finished case. The more useful starting point is the maximum packed product envelope, followed by the intended loading arrangement.
Nominal product dimensions can also hide real variation. A cigarette may run slightly longer, a pre-roll closure may become wider, or a paper wrap may add local thickness. Accordingly, the controlling dimensions should represent the agreed maximum packed condition rather than one ideal sample.
Internal usable dimensions matter more than outside dimensions when capacity is being calculated. Hinges, rolled edges, lid curls, shoulders, and other formed details consume part of the internal envelope. An outside drawing should therefore never be used directly to estimate stick count.
Pack orientation is another early decision. Straight sticks can sit in one row, several rows, or stacked layers. Meanwhile, tapered products can use parallel or alternating directions, and each pattern creates a different width requirement.
Which Packaging Projects Need This Sizing Method?
The method is especially useful when a fixed number of cigarettes or pre-rolls must fit a compact metal format. It also helps when a flexible pouch or paper pack is moving into rigid packaging. In that situation, the previous outside dimensions may not translate into the same usable capacity.
Insert-based projects benefit for another reason. Tray walls and pocket geometry can change the cavity after the shell has already been selected. Meanwhile, loose-fill projects need a similar review when target mass, presentation, and carry thickness must stay balanced.
Existing molds can also be evaluated through this process. A current structure may work when maximum product dimensions, count, insert, removal path, and outside envelope all fit together. If several of those conditions fail, changing the package dimensions may be more practical than forcing the contents into an unsuitable cavity.
Length Sets One Axis; Count Sets the Others
Sizing for Cigarette Length and Pack Count
For straight cigarettes, maximum stick length normally establishes the minimum long dimension of the usable cavity. Still, cigarette tin dimensions cannot be selected from length alone. Pack count determines row width, while the number of layers influences cavity depth.
A useful early layout shows every stick in plan view at the maximum agreed cross-section. Working clearance is then added around the complete row. The goal is repeatable loading without forcing wrapped products against formed metal edges.
The section view answers another question. It should show the highest loaded point, any liner below the sticks, and the lowest lid feature above them. This view often identifies vertical interference that cannot be seen from a simple length-and-width calculation.

Pack Count Is a Layout Question
Multiplying nominal cigarette diameter by the required count is useful for an initial estimate. However, wrappers can vary, seams can touch, and cylindrical sticks may settle differently in a tight row. The calculation should therefore create the first layout rather than release the final drawing.
Row pattern matters as much as total count. A single layer creates a shallow profile, while stacked layers reduce footprint at the cost of extra depth. A strict pocket thickness may therefore favor a wider single-layer arrangement.
Orientation can change the opening experience as well. Longitudinal placement normally follows the long axis of a rectangular case. By contrast, another arrangement may shorten the removal path while requiring more width.
Check Removal Before Increasing Capacity
A cavity can pass a capacity check and still fail during normal use. For example, the center cigarette may sit so tightly between neighboring sticks that one item cannot be lifted cleanly. A small access gap, lifting paper, or changed row pattern can solve the problem without enlarging the complete package.
End clearance also deserves attention. Too little space can make loading sensitive to product length variation. Conversely, excessive clearance allows more movement and can make an otherwise compact format unnecessarily large.
“Fits” and “packs well” are different standards.
A piece that can be pushed into position has not necessarily passed a loading test. The complete count should load, close, open, and remove without repeated force or rearrangement.
Taper Changes the Geometry
Sizing for Pre-Rolls and Inserts
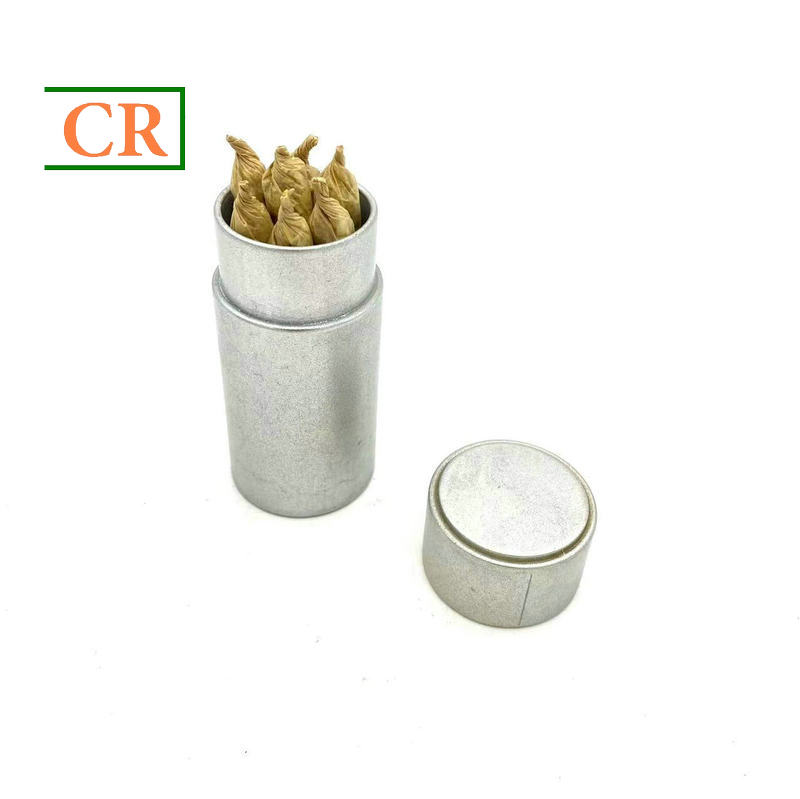
Pre-rolls create a different dimensional problem because one end may be wider than the other. The closed end can also vary in shape and height. Consequently, pre roll pack count should always be linked to orientation and maximum profile rather than product length alone.
The widest section generally controls lane spacing in an insert. At the same time, the narrow end needs enough support to avoid uncontrolled movement. A pocket designed around one nominal diameter can pinch larger samples while allowing smaller pieces to rotate.
Orientation can also change the number of pieces that fit. Parallel loading places all wide ends in a similar zone. Alternatively, opposing directions can redistribute those wider sections, although a real loading sample should confirm whether that arrangement remains practical.
Count the Complete Insert Envelope
Insert space includes more than the visible product pockets. Tray walls, bridges, pocket radii, flanges, base thickness, and finger-access zones all consume room. Once those details are added, the same metal cavity may hold fewer pieces than the original loose-product layout suggested.
Vertical space changes at the same time. A raised tray moves the packed product closer to the lid, while a deep pocket can make removal difficult. The metal shell and insert should therefore be reviewed together in both plan and section views.
|
Lane Width Measure the widest zoneCheck maximum diameter, closure shape, and local variation across representative packed pieces. |
Tray Outline Reserve the edge zonesInclude retention walls, flanges, spacing, and access features in the overall insert envelope. |
Removal Test every positionCenter, edge, and hinge-side pieces should all lift without pulling adjacent products from position. |
What Happens When the Insert Is Added Too Late?
A common development problem appears when the metal shell is selected before tray geometry is defined. After insert walls and pockets are added, the outer lanes can sit too close to the metal sides. Meanwhile, the highest product points may enter the lid clearance zone.
Access can fail even when count still works. Five pieces may fit neatly on screen, yet the center item cannot be lifted without disturbing the two beside it. In that situation, changing pocket geometry can be more effective than enlarging the whole case.
A project without a rigid tray still needs an internal-packaging allowance. Paper wraps, dividers, liners, and lifting sheets can affect both row width and stack height. “No insert” should therefore not be treated as “no internal component.”
Plan by Volume, Then Check Settling
Sizing for Loose Tobacco Volume and Headspace
Loose tobacco capacity cannot be planned like a row of cigarettes because the contents have no fixed outer shape. The same target mass may occupy different heights after filling and settling. A practical volume trial should therefore accompany any weight target.
Begin with representative material and the intended filling method. Record the initial fill height, settle the sample using a repeatable handling method, and measure the level again. The difference shows how apparent volume may change without any change in product mass.
Cut style and handling can also affect the occupied volume. Accordingly, one tightly compressed sample should not become the only capacity reference. A small group of representative fills gives a more useful view of the working range.
Headspace Is Working Space
Headspace is the free volume above the intended fill. Too little space can leave loose strands near the rim or closing path. By contrast, excessive free volume can make the pack appear underfilled and allow more movement after handling.
A working fill-height range is often more useful than one theoretical fill line. The upper condition should still allow the case to close cleanly. Meanwhile, the lower condition should remain visually and functionally acceptable after expected settling.
A useful loose-fill test
Fill the sample, close it, handle it, reopen it, and inspect the rim. Repeated material in the closure area may indicate excessive fill height, unsuitable cavity proportions, or an inconsistent filling method.
Broad and Shallow Versus Narrow and Deep
Two cavities may offer similar calculated volume while creating very different handling conditions. A broad shallow case exposes more product near the opening. Conversely, a deeper format can reduce footprint but make material at the bottom harder to reach as the fill level falls.
Internal corner geometry also changes the usable volume. A finished cavity is not a perfect rectangular block because corners and formed edges occupy part of the theoretical space. Length × width × depth is therefore an estimate rather than a final capacity guarantee.
Liners and inner bags should be present during the capacity trial. Folded material can take side space and rise above the settled fill line. The final loading check should use the complete internal packaging arrangement rather than an empty metal shell.
Capacity Must Still Feel Portable
Closure and Pocket-Portability Trade-Offs
Closure geometry takes real space and changes the effective opening. Hinges, rolled edges, lid curls, shoulders, and other formed details can reduce clear access near the walls. Similar outside dimensions therefore do not always produce the same usable cavity.
Pocket portability introduces another trade-off. A modest increase in length or width may be less noticeable than extra thickness. Corner shape, edge profile, and closure projection also influence how a pocket tin sits in a pouch, pocket, or small secondary package.
Check the Package in Three Real Use States
The empty state shows basic opening and closing behavior. The fully loaded state checks maximum stack height, lid contact, and packed thickness. Finally, the partly used state reveals how remaining pieces or loose contents move after several removals.
A simple dimensional block can answer early portability questions before a refined metal sample exists. It can be placed in the intended carry location or secondary carton to check the overall envelope. A later production-style sample can then confirm opening travel and actual packed behavior.
When outside thickness is a hard limit, that condition should appear clearly in the dimensional brief. Capacity, insert depth, and removal clearance then become the variables available for adjustment. This priority prevents repeated drawings from optimizing a dimension that cannot actually move.
Portability Check
The smallest outside footprint is not automatically the most portable option. A slightly wider case may carry more comfortably when it avoids unnecessary thickness and still provides clean removal access.
Turn Drawing Assumptions Into Observed Behavior
Prototype Loading and Removal Tests
A prototype should answer more than whether the required contents physically enter the cavity. The test should cover loading, closing, opening, individual removal, movement, and repacking. This broader review often reveals problems that remain invisible in a CAD capacity study.
Product variation matters during the trial. Include longer sticks, wider cones, irregular closed ends, and loose-fill samples near the planned operating limits. Otherwise, one carefully selected sample can hide the condition most likely to create a fit problem.
- Load the complete count. Watch for forced alignment, snagging, crowded corners, or products rising above neighboring positions.
- Close the lid normally. Check the rim, highest packed point, insert edge, hinge side, and closure path.
- Remove products from several positions. Test center, edge, corner, and hinge-side locations rather than only the easiest piece.
- Handle the closed sample. Turn and carry it so migration, tray lift, layer shift, or uncontrolled movement becomes visible.
- Repeat after meaningful dimensional changes. A small revision can alter lane fit, lid clearance, insert retention, or removal behavior.
Record the Sample That Actually Passed
Photography can make prototype reviews easier to compare. Record the loaded top view, open-lid condition, and any difficult removal point. Meanwhile, keep the cavity and insert revision with the sample record so results from different versions are not mixed.
Pass-or-revise criteria should be agreed before final approval. Otherwise, a difficult fit may be accepted simply because the required count technically enters the case. Clear criteria keep engineering capacity and practical use connected.
Make the Request Engineering-Ready
Dimension Brief for the Supplier
A useful dimension brief describes the complete packed system rather than only the desired outside shell. Start with product format, maximum measured dimensions, required count or fill mass, and preferred orientation. Then include every insert, liner, divider, paper wrap, or accessory that shares the usable cavity.
Hard limits should be separated from preferred targets. A maximum pocket thickness may be fixed while width remains flexible. In another project, a display footprint may be locked while depth can still change slightly.
Information to Include
- Packed format: straight cigarette, tapered pre-roll, tube, loose leaf, or mixed set
- Maximum product length, width, diameter, taper, or irregular profile
- Required piece count or target loose-fill mass
- Preferred orientation, row pattern, and layer count
- Insert type, tray outline, pocket concept, liner, divider, or paper wrap
- Required finger access, lifting feature, refill method, or full-pack removal method
- Headspace or tested fill-height range for loose contents
- Maximum outside length, width, depth, or pocket thickness where fixed
- Closure preference and any separately defined performance requirement
- Representative samples when available
Existing Size or Custom Adjustment?
An existing structure is worth considering when the maximum product fits with workable clearance. The required count should still fit after inserts and liners are included. Removal, outside proportions, and the intended carry profile should also remain acceptable.
A size adjustment becomes more relevant when capacity is repeatedly compromised. The same applies when an insert cannot fit, unnecessary empty volume remains, or outside thickness misses a defined portability target. In those cases, forcing the packed format into an existing cavity can create more compromises than it removes.
Existing structures can be compared on the metal packaging product range. These product pages provide structural references before a dimensional brief is narrowed. Final suitability should still be checked with the actual packed format.
Practical Purchasing Checks
A useful sourcing comparison should place capacity beside usability rather than comparing outside dimensions alone. For example, a smaller shell can appear attractive on a specification sheet but become inefficient if the insert reduces count. Likewise, a larger shell may offer little benefit when the extra volume does not improve loading or removal.
Sample planning should also match the decision that needs to be made. An early dimensional mock-up can compare footprint and thickness. Later, a representative metal sample is more useful for checking the complete packed condition and opening behavior.
Artwork should follow the agreed structure rather than drive the cavity decision too early. Once size, opening direction, and insert position are stable, graphic work can use the correct viewing orientation and panel proportions. This sequence reduces unnecessary revisions between packaging engineering and artwork preparation.
Keep regulatory review separate from dimensional review.
Package dimensions alone do not establish market compliance. For U.S. tobacco products, current labeling and warning requirements should be reviewed against official FDA tobacco-product guidance. Cannabis pre-rolls may be subject to separate state-level packaging and labeling rules, including child-resistant packaging requirements.
Keep Measurements Consistent
One controlling unit system should remain consistent across drawings and the dimensional brief. When a second unit is shown for convenience, the original measured values should stay as the reference. Rounded conversions can otherwise accumulate small differences across several packed positions.
Physical samples are particularly useful for tapered or irregular products. When samples are unavailable, maximum dimensions and expected variation should be described clearly. Prototype loading then becomes even more important before the final cavity is approved.
Common Sizing Questions
FAQ
Should a cigarette tin be sized by cigarette length or pack count?
Both inputs control different dimensions. Maximum cigarette length normally determines the long internal axis, while pack count determines row width and layer depth. Loading and removal clearance should then be confirmed with representative samples.
Should capacity be calculated from outside or inside dimensions?
Capacity should be evaluated from the usable internal cavity. Outside dimensions include formed metal features that do not become product space. A finished cavity or approved internal drawing provides a better basis for loading calculations.
How does an insert change capacity?
An insert consumes space through its base, walls, pockets, flanges, radii, and finger-access areas. A cavity that holds loose pieces may therefore lose capacity once a tray is added. The insert and metal shell should be reviewed together.
Why does loose tobacco need a different planning method?
Loose fill changes occupied volume as it settles and redistributes. Target mass remains important, yet volume trials and practical headspace are needed to check closing and fill presentation. A theoretical cubic calculation does not show those changes.
When is a loading sample necessary?
A loading sample is especially useful when clearances are tight, an insert defines the layout, or product variation is significant. It also matters when a strict outside size leaves little room for adjustment. The sample should confirm loading, closing, opening, removal, and movement.
Before the Drawing Is Frozen
Three Actions That Reduce Sizing Risk
Reliable packaging dimensions begin with the contents and work outward. Straight cigarettes, tapered pre-rolls, and loose leaf each require a different capacity model. Even so, all three benefit from maximum-sample measurements and a physical loading review.
- Measure the maximum packed product. Use realistic variation rather than one nominal sample.
- Map the complete internal stack. Include inserts, liners, headspace, removal access, and closure movement.
- Test the complete use cycle. Confirm loading, closing, opening, removal, and carry behavior before outside dimensions are frozen.
Next Step
Send Product Dimensions for a Sizing Review
Prepare the packed format, maximum dimensions, required piece count or fill mass, insert concept, and portability target. When available, add representative samples and any hard limit on outside length, width, or thickness.
With those inputs, a tobacco tin can be evaluated around real loading conditions rather than appearance alone. The next discussion can focus on usable cavity size, insert space, headspace, removal access, closure movement, and whether an existing structure or adjusted size is the better starting point.
| Send Product Dimensions → | Compare Tin Structures |
Post time: Oct-28-2026