A metal box often feels simple until the first physical sample arrives. A broad lid may flex when pressed, a corner may pick up a shallow dent during packing, or a heavier sheet may make the lid feel less natural when opening. None of these results can be predicted from thickness alone. The finished structure depends on panel size, shape, lid overlap, forming depth, edge construction, internal support, and the way the box moves through filling and transport.
The practical answer
Thickness should solve a defined structural problem, not simply make the specification look heavier.
Start with the area that actually looks or feels wrong: the center of a wide lid, a long sidewall, a hinge edge, a deep-drawn corner, or a surface that receives repeated packing pressure. Then compare material and structural changes against that specific weakness.
|
What you notice Lid flex, dents or poor closure feel |
→ |
What to check Panel span, edge support and contact points |
→ |
What to compare Gauge change versus structural change |
Consider a gift tin displayed on a retail shelf. The pack may look perfectly flat when empty, yet the lid can flex after several units are stacked inside a carton. In another project, a compact hinged case may feel much firmer even though the nominal sheet thickness is identical. The difference comes from geometry rather than the number printed on the material specification.
This is why thickness selection belongs inside the structural design process. Material, lid construction, forming features, and real handling conditions need to work together when developing custom tin packaging structures.
Start with what the number means
What Tinplate Thickness Can and Cannot Tell You
Tinplate thickness describes the nominal gauge of the sheet before it becomes a finished box. A thicker sheet normally offers more resistance to local bending. However, that statement only describes the raw material, not the final three-dimensional structure.
Once the blank enters forming tools, the situation changes. Corners become curved. Edges become rolled. Sidewalls rise from the flat sheet. A lid gains a skirt and sometimes a bead, embossing, hinge, or stepped profile. These features redirect force and change how the finished metal behaves.
Why panel span changes the result
|
Wide unsupported panel A longer span gives the center more room to move. |
VS |
Short supported panel A shorter span limits movement before gauge changes. |
Why a wide lid can feel softer
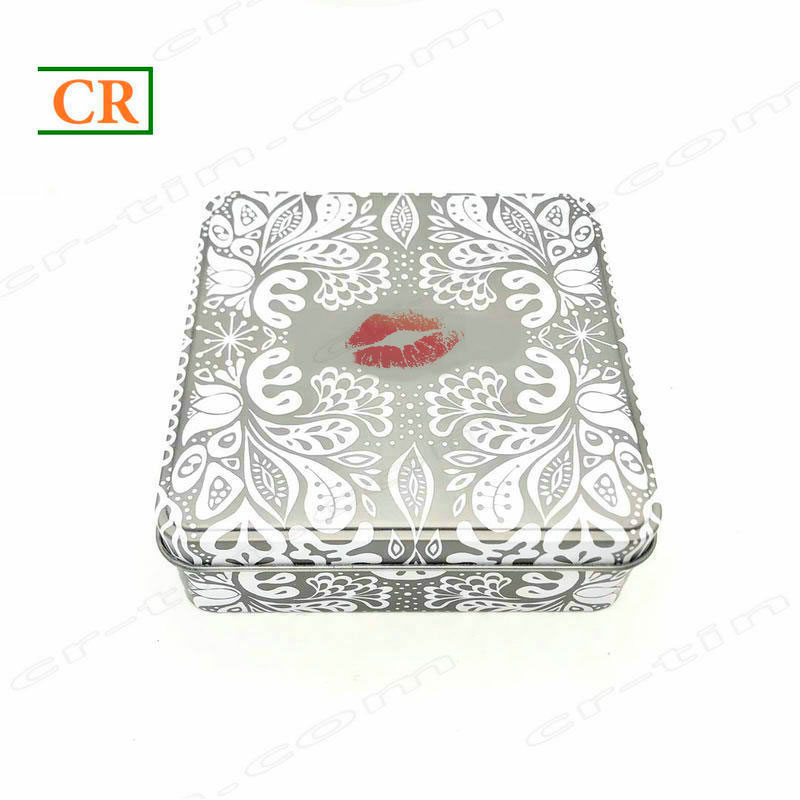
Imagine pressing the middle of a large square biscuit tin. The nearest supporting edge may sit several centimeters away. That open span gives the sheet room to move, so the center can flex even when the corners feel strong.
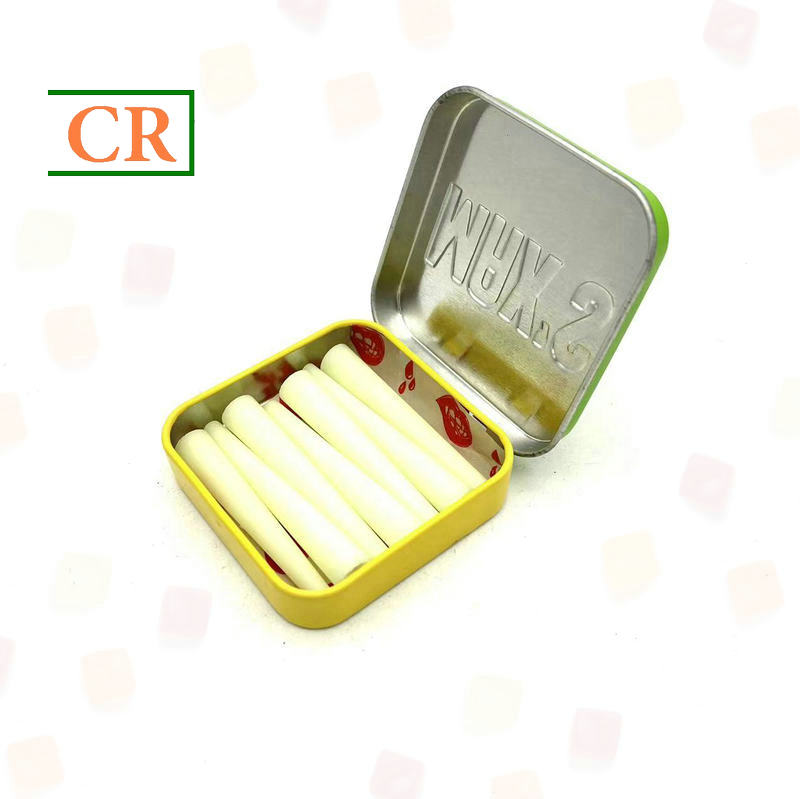
Now compare that experience with a small mint case. The fingers are much closer to the edges, while the short walls and rounded corners create additional support. The smaller box can therefore feel surprisingly solid without relying on a dramatic change in gauge.
Temporary flex is different from a dent
A lid that moves slightly under pressure is not automatically failing. The more important question is what happens after the pressure disappears. Some panels spring back cleanly. Others keep a shallow dish, crease, or corner mark.
|
Temporary flex The panel moves under pressure and returns without leaving a visible permanent mark. |
Permanent dent The surface keeps a dish, crease or local mark that affects shelf appearance. |
That distinction matters for decorative metal boxes. A pack may still protect the contents while looking damaged under shelf lighting. Surface appearance therefore becomes part of structural performance, especially on large glossy or metallic panels.
The shape changes the result
How Size, Shape, Lid and Forming Affect Rigidity
A thickness number becomes meaningful only after the box shape is known. Square, rectangular, round, shallow, and deep-drawn formats all distribute pressure differently. Even two square boxes can behave differently when one is twice the width of the other.
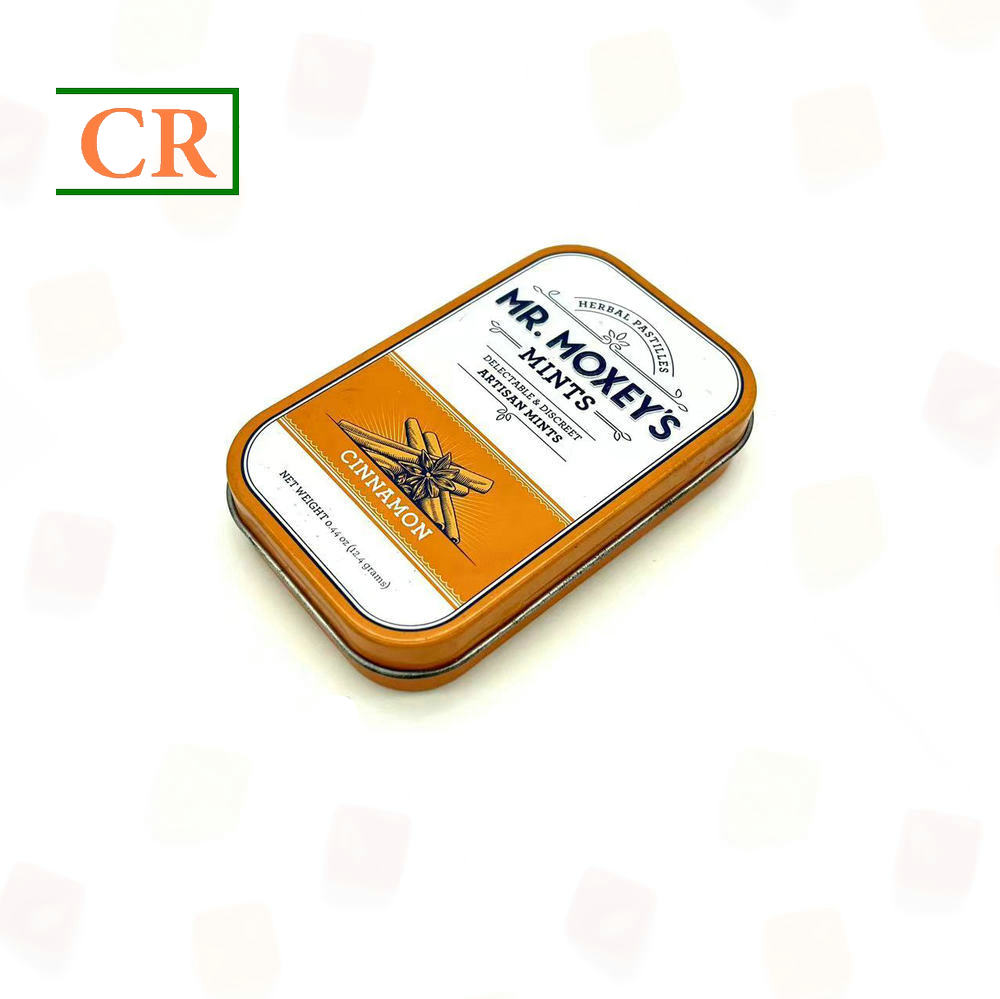
The three CR Tin structures below make that difference easier to see. They are visual references rather than universal material rules. Their proportions, lid systems, and panel spans create different engineering conditions.
Panel width changes what the hand feels
A broad lid has a longer unsupported distance between its edges. When pressure reaches the middle, that distance allows more movement. A smaller lid reduces the span, so the material has less room to deflect.
This effect becomes even more noticeable on long rectangular formats. The panel may feel firm across its short direction but softer along the longer direction. That is why a single squeeze near one corner says very little about the complete structure.
Edges, beads and lid skirts quietly do a lot of work
A rolled edge changes a thin sheet into a much stiffer perimeter. A shallow step can reduce the effective flat area. Likewise, a bead or shoulder can redirect flex away from the center of the panel.
| Rolled edge Stronger perimeter |
Bead or step Shorter effective span |
Deeper lid skirt Better edge support |
These details often explain why two tins with similar material can feel very different. They also create opportunities to improve strength without increasing sheet thickness across every surface.
Deep forming changes the conversation
A shallow lid mainly raises questions about panel flex. A deep-drawn body introduces another issue: the metal must travel farther through the forming tool. Corners, walls, shoulders, and narrow radii begin to control the result.
At that stage, heavier material is not automatically easier. More material can increase resistance during forming and change springback. The finished sample needs to show both structural stability and clean forming.
Reference points, not fixed answers
Thinking About 0.21, 0.23, 0.25 and 0.28 mm
When a supplier proposes values such as 0.21, 0.23, 0.25, or 0.28 mm, treat them as candidates rather than application rules. Each change affects material mass and bending resistance, while the finished result still depends on the surrounding geometry.
The better question is not “Which thickness is strongest?” but “What problem should the next thickness solve?”
| 0.21 mm Compact or well-supported structures. |
0.23 mm A practical comparison reference. |
0.25 mm More local resistance where justified. |
0.28 mm Use only when the structure gives a clear reason. |
| Gauge | Why compare it | Possible benefit | Still check |
|---|---|---|---|
| 0.21 mm | Compact or well-supported format. | Lower material mass. | Wide panels, dents and visual waviness. |
| 0.23 mm | Conventional formed structures. | Balanced comparison point. | Panel span, lid design and transport contact. |
| 0.25 mm | A defined area needs more resistance. | More material against bending. | Springback, closure, fit and forming load. |
| 0.28 mm | A demanding structure has a clear reason. | Greater material resistance. | Tight forming, curls, weight and economics. |
Exact material gauges should be confirmed for the specific project and approved against the finished structure rather than treated as universal stock specifications.
0.21 mm: A lighter candidate makes more sense when the format is compact or the structure already provides useful support. Reducing thickness, however, can make cosmetic waviness or shallow dents easier to notice on broad printed surfaces.
0.23 mm: Several existing CR Tin structures provide examples around this nominal value, yet their sizes and lid systems produce different results. The useful question is why a particular 0.23 mm structure works—not whether the number should become a universal rule.
0.25 mm: Moving upward should create an observable benefit. The heavier sample still deserves a full opening and closing check because springback and mating clearance can also change.
0.28 mm: A heavier gauge can make sense when a larger or demanding structure has shown a clear need. Extra thickness cannot rescue every weak design, so large unsupported spans may still be better addressed through geometry.
What happens after the sample leaves the desk
Dent Risk, Forming Risk and Real Handling Conditions
A metal box rarely experiences one clean, centered load. During packing, one corner may touch a divider. During warehousing, the master carton may carry vertical pressure. During parcel delivery, the box can experience repeated changes in orientation.
These everyday conditions explain why hand squeezing alone gives an incomplete picture. Real dent risk depends on where force enters the structure and how concentrated that force becomes.
|
Retail shelf Appearance becomes performanceA shallow dent can become obvious when light moves across a large glossy lid. |
Master carton Pressure becomes localDivider edges and neighboring tins can create concentrated contact points. |
Filling line Contact becomes repetitiveGuide rails, belts and pushers may repeatedly touch the same sidewall. |
The weak spot is often predictable
A broad lid usually directs attention toward its center. A hinged case adds the hinge side and opening edge. A tall drawn body shifts attention toward corners and walls. Mapping those areas before sampling makes the physical review far more useful.
This does not require an elaborate laboratory program at the early stage. Even a consistent side-by-side handling comparison reveals more than random squeezing. The important point is to press, carry, stack, and open each version in the same way.
Secondary packing can change the answer
A fitted paper sleeve can protect sidewalls from direct contact. A molded insert can support the contents and sometimes reduce inward wall movement. Meanwhile, loose metal boxes inside a carton may strike one another during transport.
For this reason, the final pack-out should appear in the thickness discussion. Evaluating the metal shell without its real packing environment can lead to a heavier specification than necessary—or a structure that performs well only before shipment.
Balance material with design
When to Add Material—and When to Change the Structure
A thickness increase adds metal across the full blank, even when only one area needs help. On a large lid, that extra mass can become meaningful across an entire production run. Yet simply choosing the lightest possible gauge can also create hidden costs through dents, rework, or additional protective materials.
|
Consider more thickness when The material itself is the weak link
|
Consider geometry when The unsupported span is the real problem
|
A better question than “Can the sheet be thicker?”
Describe what actually looks or feels wrong. “The center of the lid stays slightly dished after case packing” gives a clear engineering target. “The box needs to feel stronger” does not.
A shallow perimeter step can shorten a flat span. A small bead can control flex. A deeper lid skirt can improve edge support. Each option changes the structure locally instead of adding material everywhere.
Of course, those changes affect appearance too. A premium lid designed around a clean uninterrupted illustration may not suit a visible rib. In that situation, changing gauge can become the more appropriate choice.
Good structural selection is rarely about one rule. It is a balance between touch, appearance, forming, packing, weight, and the visual language of the brand.
Make the sample answer one clear question
Use Samples to Isolate the Real Cause
A physical sample becomes much more valuable when the reason for making it is clear. One version may answer whether the lid needs more stiffness. Another may test whether a new rib solves the same problem without extra material.
Changing several features at once makes the result difficult to read. If gauge, lid depth, embossing, and corner radius all change together, a better sample does not reveal which change delivered the improvement.
|
Sample A Keep the structure unchanged Change only the realistic gauge being evaluated. |
↔ |
Sample B Compare under the same handling Stack, press, open and inspect both versions in the same way. |
Bring the real product and pack-out into the discussion
An empty tin does not always behave like a filled one. A fitted insert may support the walls. A dense product can create its own pressure points. Loose contents may repeatedly strike the inside surface during distribution.
The master carton matters as well. Unit orientation, dividers, carton fit, stacking direction, and transport route help explain which panels need the most protection.
What should remain attached to the approved sample
Once the final structure performs as intended, the material gauge should remain tied to the approved drawing and sample revision. Critical closure dimensions, formed details, and appearance references can then follow the same revision.
- Record the approved material gauge with the drawing revision.
- Keep a physical reference when dent appearance or flatness is visually important.
- Identify lid, hinge, curl, corner, or wall dimensions that affect fit.
- Retain the pack-out arrangement used during the handling review.
- Recheck the structure when material, tooling, dimensions, or key forming details change.
A practical decision path
From First Weak Spot to Approved Structure
| 01 Find the weak area Flex, dent, forming mark or closure issue. |
02 Control the comparison Change one meaningful variable at a time. |
03 Test the real pack Include contents, inserts, carton and handling. |
04 Lock the reference Link material, drawing, sample and QC revision. |
This approach makes later changes easier to judge. If the box becomes wider, the original decision can be revisited around panel span. If the lid changes from loose-fit to hinged, attention can move toward the hinge and closure zones instead of restarting the entire material discussion.
Common structural questions
FAQ
Is thicker tinplate always stronger?
A thicker sheet normally provides more material to resist bending. However, finished strength also depends on panel span, edges, curves, lid construction, forming quality, and the location of the applied force.
Can the same thickness suit every tin size?
No fixed gauge should be assumed across every size. A wider lid creates a longer unsupported span, while compact curved or hinged structures can distribute pressure very differently.
How should dent resistance be checked?
The most useful checks reproduce likely pressure locations. Lid centers, long sidewalls, corners, hinge zones, carton contact, and repeated opening can all reveal different weaknesses.
When must a thickness value be reconfirmed?
A material change is the obvious trigger. Structural changes can also justify another check, especially when dimensions, draw depth, lid geometry, embossing, tooling, or packing conditions affect the assumptions behind the approved sample.
Before the material is locked
A good thickness decision should survive three questions.
Does it solve the actual weak area? Does it still work with the real product and pack-out? Can the approved gauge, drawing and physical sample remain tied together as one QC reference? If the answer is yes, thickness has become a controlled structural decision rather than an isolated purchasing number.
Next step
Compare the Structure Before Locking the Gauge
For a useful sample review, provide the box shape, dimensions, intended contents, lid style, formed details, internal support, filling method, secondary packing, and expected transport conditions. These details create a practical basis for comparing rigidity, dent sensitivity, forming behavior, and opening feel.
You can also review existing tin packaging structures before deciding which material direction should be sampled.
Post time: Sep-14-2026